octubre de 2026
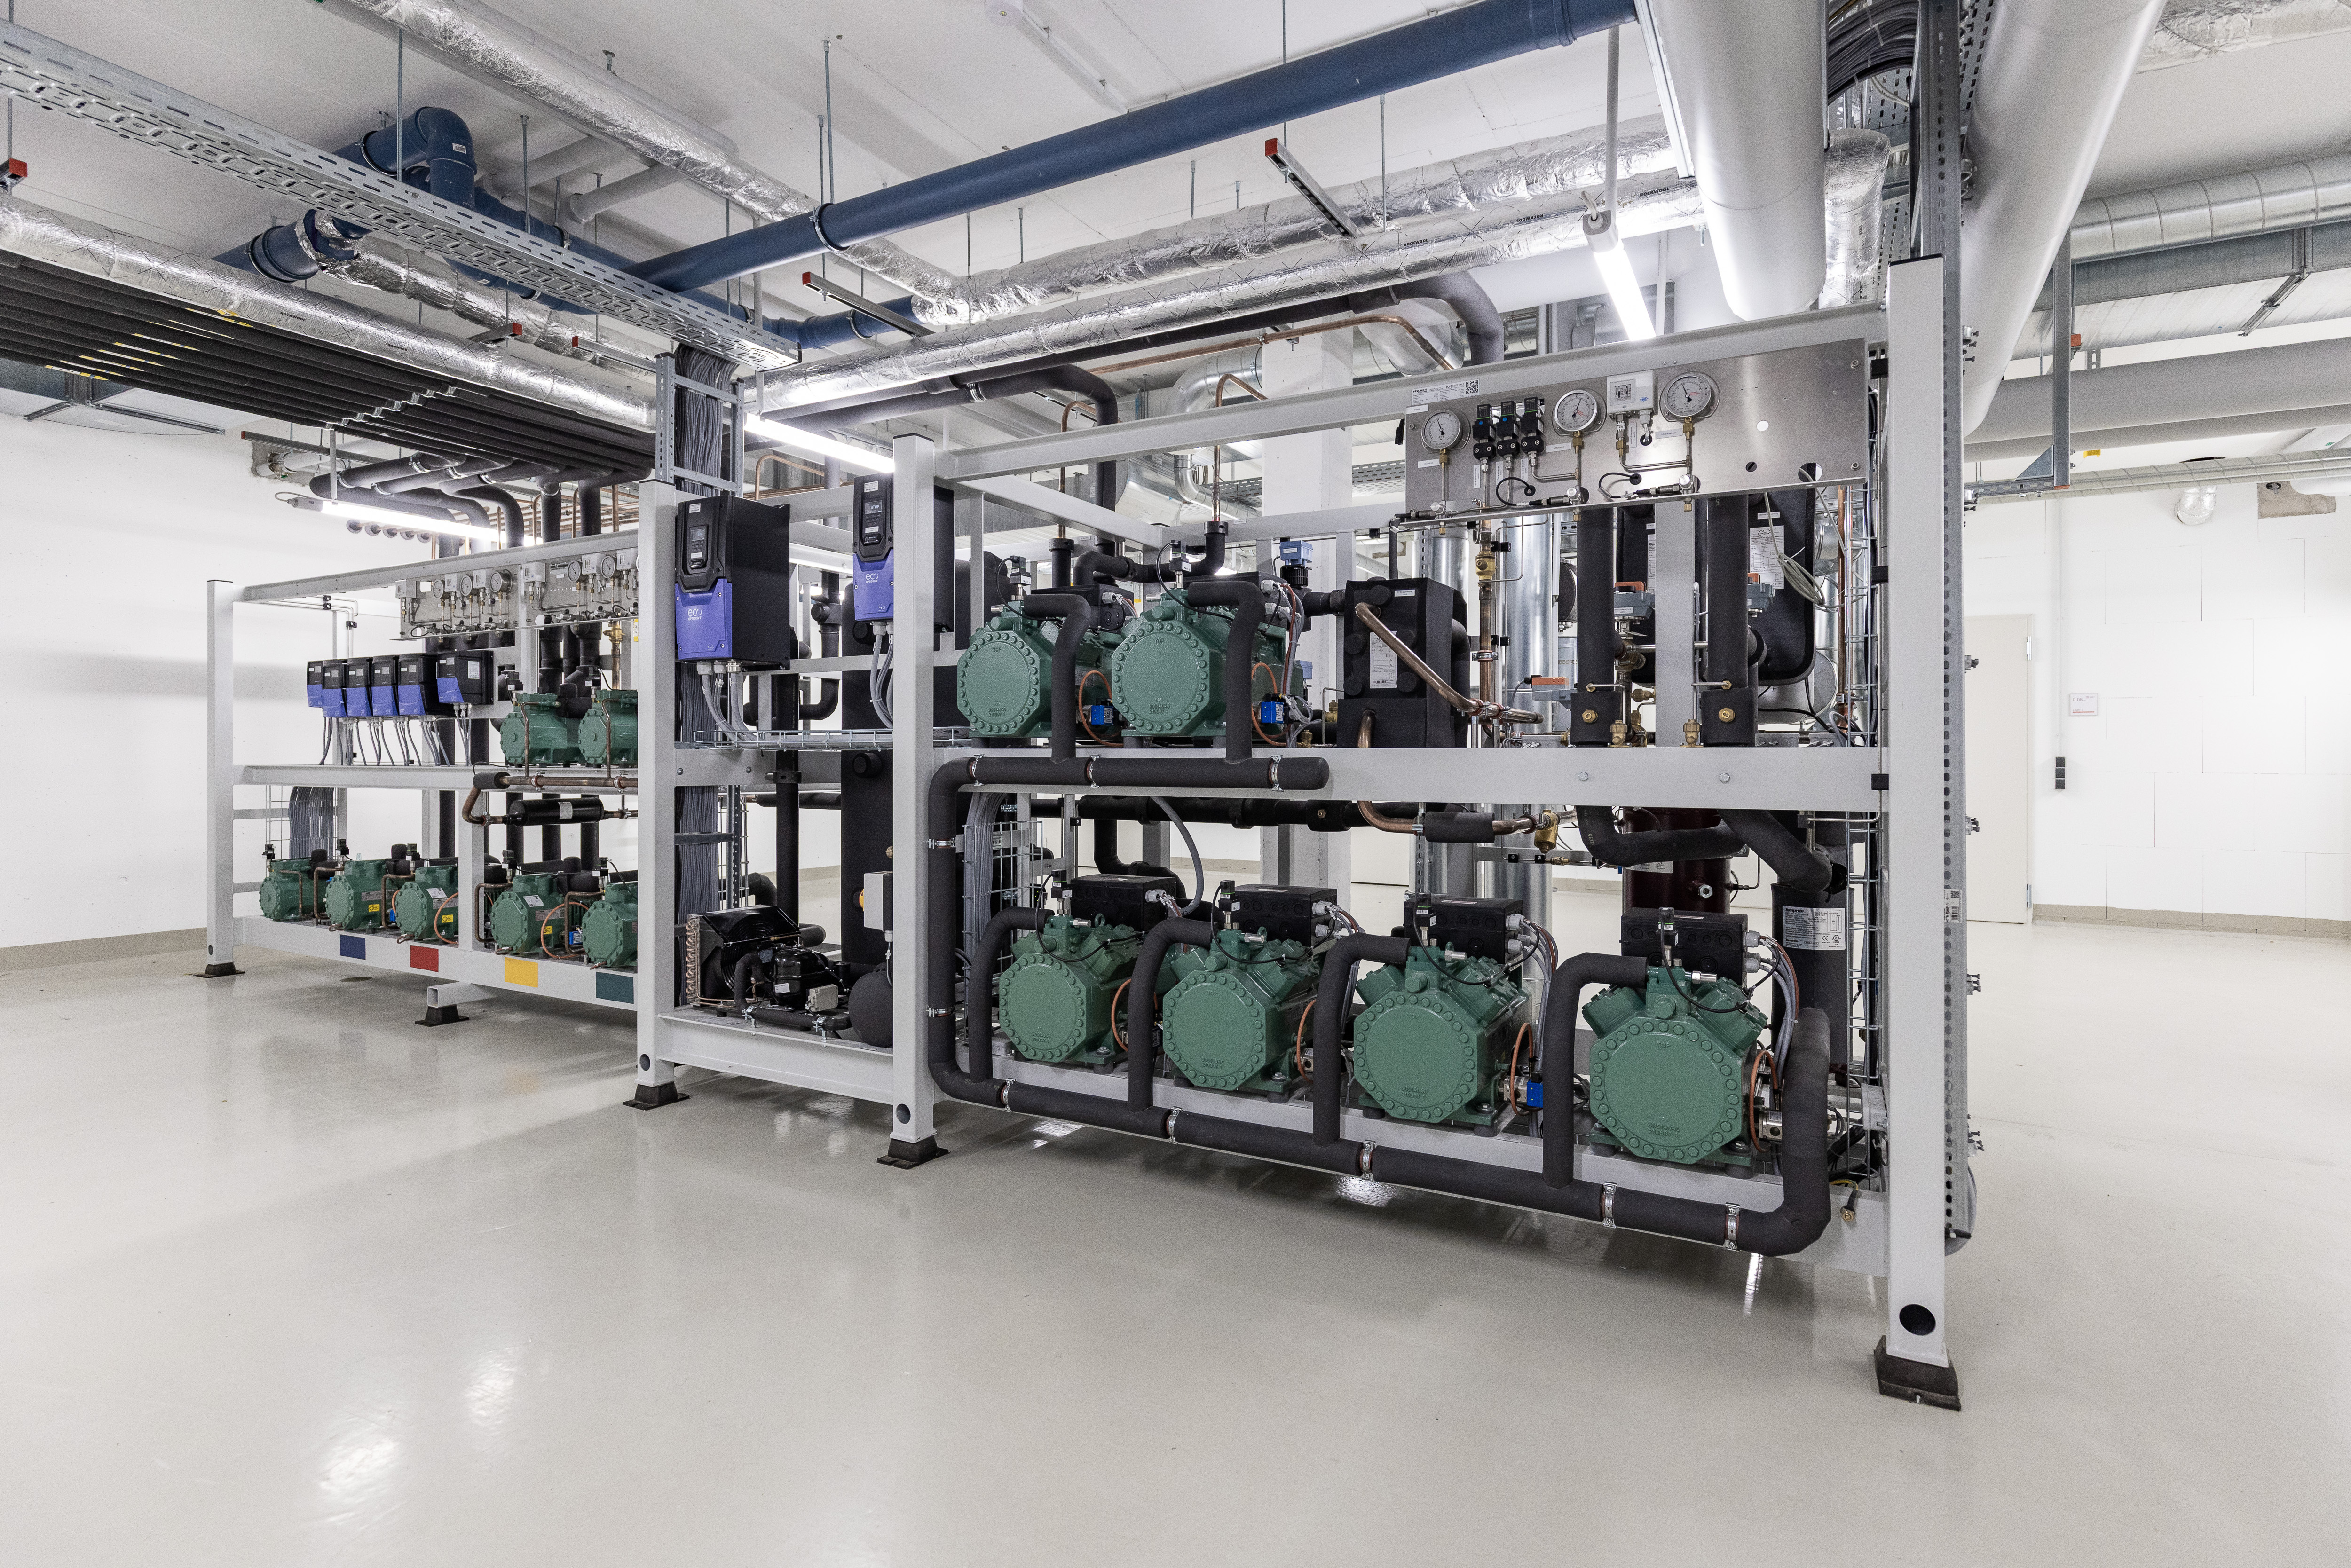
A CO₂ booster system from [CF] SYSTEMS reliably supplies the new regional kitchen of the Evangelische Heimstiftung in Neuenstadt with refrigeration for storage, rapid cooling and blast freezing. A total of 13 reciprocating compressors from the BITZER ECOLINE CO₂ series provide the required refrigerating capacity for the demanding cook-and-chill processes. The system combines natural refrigeration technology, differentiated controllability and heat recovery to create a future-proof solution for a modern large-scale kitchen.
Application
Sector alimentario
Location
Germany
Focus Product
ECOLINE SL Series
Refrigerant
Refrigerantes naturales
Technical Opportunity
From the gentle preparation of meals to their safe storage, refrigeration technology plays a central role in the new regional kitchen in Neuenstadt operated by Evangelische Heimstiftung GmbH. With the new building, EHS is strengthening its supply structure in northern Baden-Württemberg while also implementing an environmentally friendly overall concept. EHS provides care for more than 16,000 people in 170 facilities. The Neuenstadt regional kitchen is one of three production kitchens and supplies up to 10,000 meals every day. Construction began in spring 2024, the construction period was around one year, and the investment amounted to approximately €20 million.
Process refrigeration for demanding applications
Production at the regional kitchen is based on the cook-and-chill process. Meals are approximately 90% pre-cooked and then rapidly cooled to 3°C within 60 to 90 minutes. For special applications, a freezer is also available that enables temperatures down to –30°C. This application therefore places high demands on the refrigeration technology: peak loads must be handled reliably, defined cooling curves must be maintained consistently, and availability during continuous kitchen operation must be ensured at all times.
The refrigeration supply covers both storage and process cooling. The scope of supply includes cold rooms with a total area of approximately 695 m², distributed across 14 rooms. In total, the consumer structure comprises 19 medium temperature refrigeration points, three low temperature cold rooms, four rapid coolers and one blast freezer. The rapid coolers and freezer were integrated into the cold rooms with customised enclosures so that work routes and material flows are not affected.
BITZER compressors at the heart of the high-performance system
The centrepiece of the refrigeration supply is a CO₂ booster system from [CF] SYSTEMS. Using the natural refrigerant CO₂ (R744), the system relies on a sustainable and long-term future-proof solution. A total of 13 reciprocating compressors from the BITZER ECOLINE CO₂ series provide the required refrigerating capacity: four for medium temperature refrigeration (1× 4GTE-30K and 3× 4GTE-20K), two for low temperature refrigeration (1× 2LSL-1K and 1× 2KSL-1K), four for the rapid coolers (4× 2DSL-5K), one for the blast freezer (1× 2GSL-3K) and two parallel compressors (2× 4HTE-20K).
The system design demonstrates how differentiated modern CO₂ refrigeration technology must be in responding to different process requirements. For medium temperature refrigeration, a refrigerating capacity of approximately 80 kW at t₀ = –8°C is provided, while low temperature refrigeration requires 12 kW at t₀ = –28°C. The four rapid coolers each deliver approximately 20 kW at t₀ = –28°C, and the blast freezer approximately 8 kW at t₀ = –40°C. In addition, heat recovery of 2× 90 kW is integrated. The close capacity gradation of the compressors enables precise adaptation of the refrigerating capacity to actual demand. The wide speed range further supports a high level of control accuracy.
Precise controllability for sensitive processes
A special feature of the system is operation at nine pressure levels. Each evaporation temperature has its own suction line, allowing different performance requirements of the consumers to be controlled independently without affecting other refrigeration points. This flexibility is particularly important in cook-and-chill processes because rapid cooling, low temperature refrigeration and storage simultaneously impose different requirements.
A special control concept was implemented jointly with Wurm for the rapid cooling and freezing processes. It supports a uniform cooling curve when warm products are loaded. At high suction pressures caused by very warm products, the low temperature compressors are backed up on the high-pressure side in order to ensure a uniform cooling curve, particularly for sensitive products. This keeps the reciprocating compressor within its optimum operating range. At the same time, superheating on the medium temperature suction side is significantly reduced. Increased flash gas formation and additional suction injection are avoided, improving the operational stability of the system.
All ECOLINE 4-cylinder reciprocating compressors used are equipped ex works with the IQ MODULE CM-RC-02. In addition to monitoring important operating data, the module simplifies service work and contributes to high system availability.
Making effective use of energy
A key efficiency component is the two-stage heat recovery system. This is used to heat service water and drinking water with capacities of up to 90 kW each. A Güntner Flat VARIO gas cooler GGHV with a capacity of 308 kW is installed on the roof for heat rejection. Güntner air coolers from the VARIO and COMPACT series are used in the cold rooms.
The system therefore combines reliable refrigeration supply for the large-scale kitchen with consistent utilisation of the heat generated. In this way, the refrigeration technology becomes an integral part of the overall energy concept of the new site.
Tailor-made implementation on site
The structural requirements were demanding. In order to bring the CO₂ booster system into the building, the system was manufactured in two sections and connected on site.
The kitchen was designed by Ingenieurbüro Seewöster GmbH of Wiesloch, taking into account the specific requirements relating to hygiene, processes and operational workflows. The refrigeration system was built by Götz & Klinger GmbH of Duisburg, a specialist company with more than 40 years of experience in refrigeration, air conditioning and draught beer systems as well as heat pump systems.
The project was implemented in close cooperation with the Fischer branch in Düsseldorf, with project support provided by Deputy Branch Manager Frank Teichmann. The project partners closely integrated kitchen planning, refrigeration technology and implementation.
The Neuenstadt regional kitchen demonstrates how cook-and-chill production, the natural refrigerant CO₂, differentiated pressure levels, energy-optimised control and extensive heat recovery can be combined to create a stable and climate-friendly process refrigeration solution. The 13 BITZER compressors play a central role in this: they provide the required capacity for the various temperature and process ranges and help ensure that storage, rapid cooling and blast freezing can be operated reliably in parallel.